DM Water Plant: Process, Applications & Industrial Benefits
Everything you need to know about DM (Demineralization) Water Plants—including working principles, ion-exchange processes, demineralization technologies, key benefits, industrial applications, regeneration, operation, maintenance, and water-quality considerations. Learn how DM plants effectively remove dissolved ions and mineral salts, produce high-purity water, protect boilers and industrial equipment, reduce scaling and corrosion risks, improve process efficiency, and support reliable water management for pharmaceutical, chemical, power, manufacturing, and other industrial applications.
Home / Blogs / DM Water Plant: Process, Applications & Industrial Benefits
A DM (Demineralization) Water Plant is a water treatment system designed to remove dissolved mineral salts and ionic impurities from water to produce high-purity demineralized water. It is commonly used where low-conductivity and low-mineral water is required for industrial processes, boilers, laboratories, and specialized applications. DM plants help reduce the risk of scaling, deposits, and other problems associated with dissolved ions.
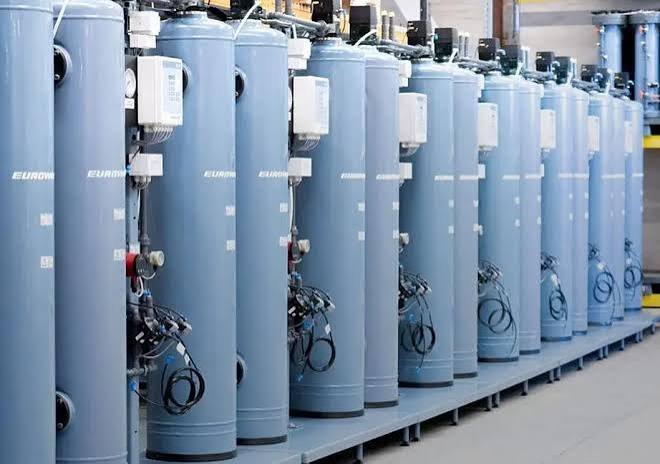
A conventional DM plant generally works through an ion-exchange process using cation and anion exchange resins. The cation unit removes positively charged ions such as calcium, magnesium, sodium, and other cations, while the anion unit removes negatively charged ions such as chloride, sulfate, bicarbonate, and silica, depending on the system configuration. In many systems, a mixed-bed unit may be used as a polishing stage to achieve higher water purity and lower conductivity.
The typical DM water treatment process includes pre-filtration, cation exchange, degassing where required, anion exchange, and polishing or mixed-bed treatment. The resins become exhausted during operation and require regeneration using appropriate chemicals. Proper regeneration, rinsing, and monitoring are important to restore resin capacity and maintain consistent treated-water quality.
DM plants provide several industrial benefits, including reduction of dissolved minerals, improved water purity, protection of boilers and process equipment, reduced scaling, improved heat-transfer performance, and reliable operation of sensitive industrial processes. The treated water can be used where mineral-free or low-conductivity water is required.
- What is a DM Water Plant?
- Why is a DM Water Plant Important?
- How Does a DM Water Plant Work?
- DM Water Treatment Process
- DM Water Plant Technologies
- Benefits and Industrial Applications of DM Water Plants
- FAQs About DM Water Plants
Quick Fact
DM Water Plants help remove dissolved mineral salts and ionic impurities, produce high-purity water, protect industrial equipment from scaling and deposits, improve process efficiency, and support reliable industrial water management.
1. What is a DM Water Plant?
A DM (Demineralization) Water Plant is a water treatment system designed to remove dissolved mineral salts and ionic impurities from water to produce high-purity, low-conductivity water. Unlike a conventional water softener, which mainly reduces calcium and magnesium hardness, a DM plant is designed to remove a much broader range of dissolved ions.
DM water is commonly required for applications where the presence of dissolved minerals can cause scaling, corrosion, deposits, conductivity problems, or process-quality issues. It is widely used for boiler feedwater, industrial processes, laboratories, pharmaceutical applications, chemical manufacturing, and other applications requiring purified water.
A conventional DM system generally uses cation and anion exchange resins. The cation exchanger removes positively charged ions such as calcium, magnesium, sodium, and other cations, while the anion exchanger removes negatively charged ions such as chloride, sulfate, bicarbonate, and other anions. A mixed-bed unit can be added as a polishing stage when very high water purity is required.
The capacity and configuration of a DM plant depend on raw-water quality, flow rate, required conductivity, silica level, application, regeneration frequency, and required treated-water quality. Proper water analysis is therefore important before designing or selecting a DM plant.
2. Why is a DM Water Plant Important?
A DM water plant is important in industries where high-purity or low-mineral water is required. Dissolved salts and minerals present in untreated water can accumulate inside boilers, heat exchangers, pipelines, process equipment, and other systems, potentially reducing efficiency and increasing maintenance requirements.
Using demineralized water helps reduce the concentration of unwanted ions and can therefore help control scale formation, mineral deposits, and conductivity-related problems. In boiler applications, appropriate water treatment is particularly important because dissolved impurities can become concentrated during operation and contribute to deposits or corrosion.
DM plants are also important for maintaining consistent process-water quality. Industries such as pharmaceuticals, chemicals, power generation, electronics, and specialized manufacturing may require water with controlled conductivity and mineral content for specific processes.
By providing consistent high-purity water, a DM plant can help protect equipment, improve process reliability, reduce maintenance requirements, support product quality, and improve overall industrial water management.
3. How Does a DM Water Plant Work?
A conventional DM plant works primarily through ion exchange. Raw water first enters the treatment system and passes through pre-treatment equipment where suspended solids and other contaminants are reduced to protect the ion-exchange resins.
The pre-treated water then passes through a cation exchange vessel. The cation resin exchanges positively charged ions in the water with hydrogen ions. This converts dissolved salts into their corresponding acids.
The water then passes through an anion exchange vessel, where anion resin removes negatively charged ions and exchanges them with hydroxide ions. The hydrogen and hydroxide ions combine to form water, resulting in significantly reduced dissolved ionic content.
For applications requiring higher purity, the water can then pass through a mixed-bed exchanger, which contains both cation and anion resins. This polishing stage can further reduce residual ions and lower conductivity.
Over time, the resins become exhausted and must be regenerated. Cation resin is typically regenerated using an acid, while anion resin is regenerated using an alkaline solution. After regeneration, the system undergoes rinsing before returning to service.
4. DM Water Treatment Process
The DM treatment process consists of several stages that work together to produce low-mineral, high-purity water.
1. Raw Water Pre-Treatment
Raw water is first treated to reduce suspended solids, turbidity, chlorine, organic matter, and other contaminants that may damage or reduce the efficiency of ion-exchange resins.
Depending on water quality, pre-treatment can include multimedia filtration, activated carbon filtration, cartridge filtration, softening, or other suitable processes.
2. Cation Exchange
Water passes through a cation exchange resin that removes positively charged ions such as:
- Calcium
- Magnesium
- Sodium
- Iron
- Other cations
The resin exchanges these ions with hydrogen ions.
3. Degassing
In some DM configurations, a degasser is installed after the cation exchanger to reduce carbon dioxide generated from bicarbonate alkalinity. This can reduce the load on the downstream anion exchanger.
4. Anion Exchange
The water passes through an anion exchange resin that removes negatively charged ions such as:
- Chloride
- Sulfate
- Bicarbonate
- Nitrate
- Other anions
The anion resin exchanges these ions with hydroxide ions.
5. Mixed-Bed Polishing
For high-purity applications, a mixed-bed vessel containing both cation and anion resins can be used. It acts as a final polishing stage and helps achieve very low conductivity.
6. DM Water Storage
The treated water is collected in a suitable storage tank and supplied to the required application. Storage and distribution systems should be designed to minimize contamination of the high-purity water.
7. Regeneration
When the resin becomes exhausted, regeneration is carried out using appropriate chemicals. The system then undergoes slow rinsing and fast rinsing before returning to service.
8. Quality Monitoring
Parameters such as conductivity, pH, silica, flow, pressure, and other application-specific water-quality parameters can be monitored to confirm system performance.
5. DM Water Plant Technologies
Different DM technologies and configurations can be selected depending on the required water purity and operating conditions.
Cation-Anion DM System
This is a conventional two-bed demineralization system consisting of separate cation and anion exchange vessels. It is widely used for industrial water treatment.
Mixed-Bed DM System
A mixed-bed unit contains both cation and anion resins in a single vessel. It is generally used as a polishing system to achieve lower conductivity and higher water purity.
Two-Bed + Mixed-Bed System
This configuration combines a cation exchanger, anion exchanger, and mixed-bed polisher. It is suitable for applications requiring higher-quality demineralized water.
Automatic DM Plants
Automatic control valves can manage service, regeneration, rinsing, and other operating cycles, reducing manual intervention and improving operational consistency.
DM + RO Integration
An RO system can be used as pre-treatment before a DM plant. RO reduces TDS and dissolved contaminants before ion exchange, which can help reduce resin loading and chemical regeneration requirements.
EDI Systems
Electrodeionization (EDI) combines ion-exchange technology with electrical processes to continuously produce high-purity water without conventional chemical regeneration. It is often integrated downstream of RO for high-purity applications.
Smart Monitoring & Automation
Modern plants can incorporate online conductivity meters, pH monitoring, flow meters, pressure sensors, PLC controls, alarms, and SCADA systems to monitor and manage plant performance.
6. Benefits and Industrial Applications of DM Water Plants
Benefits of DM Water Plants
A properly designed DM plant provides several benefits:
- Produces high-purity, low-conductivity water
- Removes dissolved ionic impurities
- Reduces mineral deposits
- Helps protect boilers and industrial equipment
- Supports consistent process-water quality
- Reduces scaling and deposit-related problems
- Improves reliability of sensitive industrial processes
- Supports efficient boiler and process-water operation
- Can be integrated with RO and other purification systems
- Supports long-term industrial water management
Industrial Applications
DM water plants are commonly used in:
- Pharmaceutical Industries
- Chemical Industries
- Power Generation Plants
- Boiler Feedwater Systems
- Textile Industries
- Food & Beverage Industries
- Automobile Industries
- Electronics & Semiconductor Industries
- Laboratories
- Engineering & Manufacturing Industries
- Cosmetic Industries
- Process Industries
Boiler Applications
DM water can be used as part of a suitable boiler feedwater treatment system where low-mineral water is required. Proper feedwater treatment helps reduce deposits and supports reliable boiler operation.
Pharmaceutical Applications
Pharmaceutical manufacturing requires carefully controlled water quality. DM systems can form part of a broader purification process depending on the required water grade and applicable standards.
Manufacturing Applications
Many industrial processes require water with controlled mineral content to prevent deposits, contamination, and process inconsistencies.
7. FAQs About DM Water Plants
1. What is DM Water?
DM water means demineralized water. It is water from which a significant portion of dissolved ionic minerals and salts have been removed through processes such as ion exchange or other demineralization technologies.
2. What does a DM plant remove?
A DM plant is designed to remove dissolved cations and anions, including calcium, magnesium, sodium, chloride, sulfate, bicarbonate, and other ionic impurities. The exact removal performance depends on system design and water chemistry.
3. What is the difference between a DM plant and an RO plant?
An RO plant uses a semi-permeable membrane to reduce TDS, dissolved salts, and many other contaminants. A DM plant primarily uses ion-exchange resins to remove dissolved ions. In many industrial systems, RO and DM technologies can be combined.
4. What is the difference between a water softener and a DM plant?
A water softener primarily exchanges calcium and magnesium hardness ions, while a DM plant removes a much broader range of dissolved ionic impurities. Therefore, softening and demineralization serve different treatment objectives.
5. Why is a mixed-bed unit used?
A mixed-bed unit contains both cation and anion resins and is generally used as a polishing stage to achieve very low conductivity and higher-purity water after primary demineralization.
6. How often does a DM plant require regeneration?
Regeneration frequency depends on raw-water ionic load, flow rate, resin capacity, water consumption, and required treated-water quality. Higher impurity loading generally results in more frequent regeneration.
7. Which chemicals are used for regeneration?
Conventional DM systems typically use an acid for cation resin regeneration and an alkaline chemical for anion resin regeneration. The exact chemicals, concentrations, and operating procedures depend on the plant design and resin manufacturer recommendations.
8. Can RO be used before a DM plant?
Yes. RO can be used as pre-treatment to reduce TDS and dissolved contaminants before ion exchange. This can reduce the ionic load on the DM system and potentially reduce regeneration requirements.
9. What parameters should be monitored in a DM plant?
Common parameters include conductivity, pH, flow rate, pressure, silica, feed-water quality, treated-water quality, and regeneration performance. The exact monitoring requirements depend on the application.
10. Where are DM plants commonly used?
DM plants are used in pharmaceutical, chemical, power, textile, food and beverage, electronics, automobile, laboratory, manufacturing, and process industries, particularly where low-mineral water is required.
Build a Better Future with Smarter DM Water Treatment Solutions
Discover advanced DM Water Plant solutions designed to produce high-purity demineralized water, remove dissolved ions and mineral salts, protect boilers and industrial equipment, reduce scaling, improve process efficiency, and support reliable long-term industrial water management.